- This topic is empty.
-
AuthorPosts
-
2026-09-14 at 2:50 pm #11446
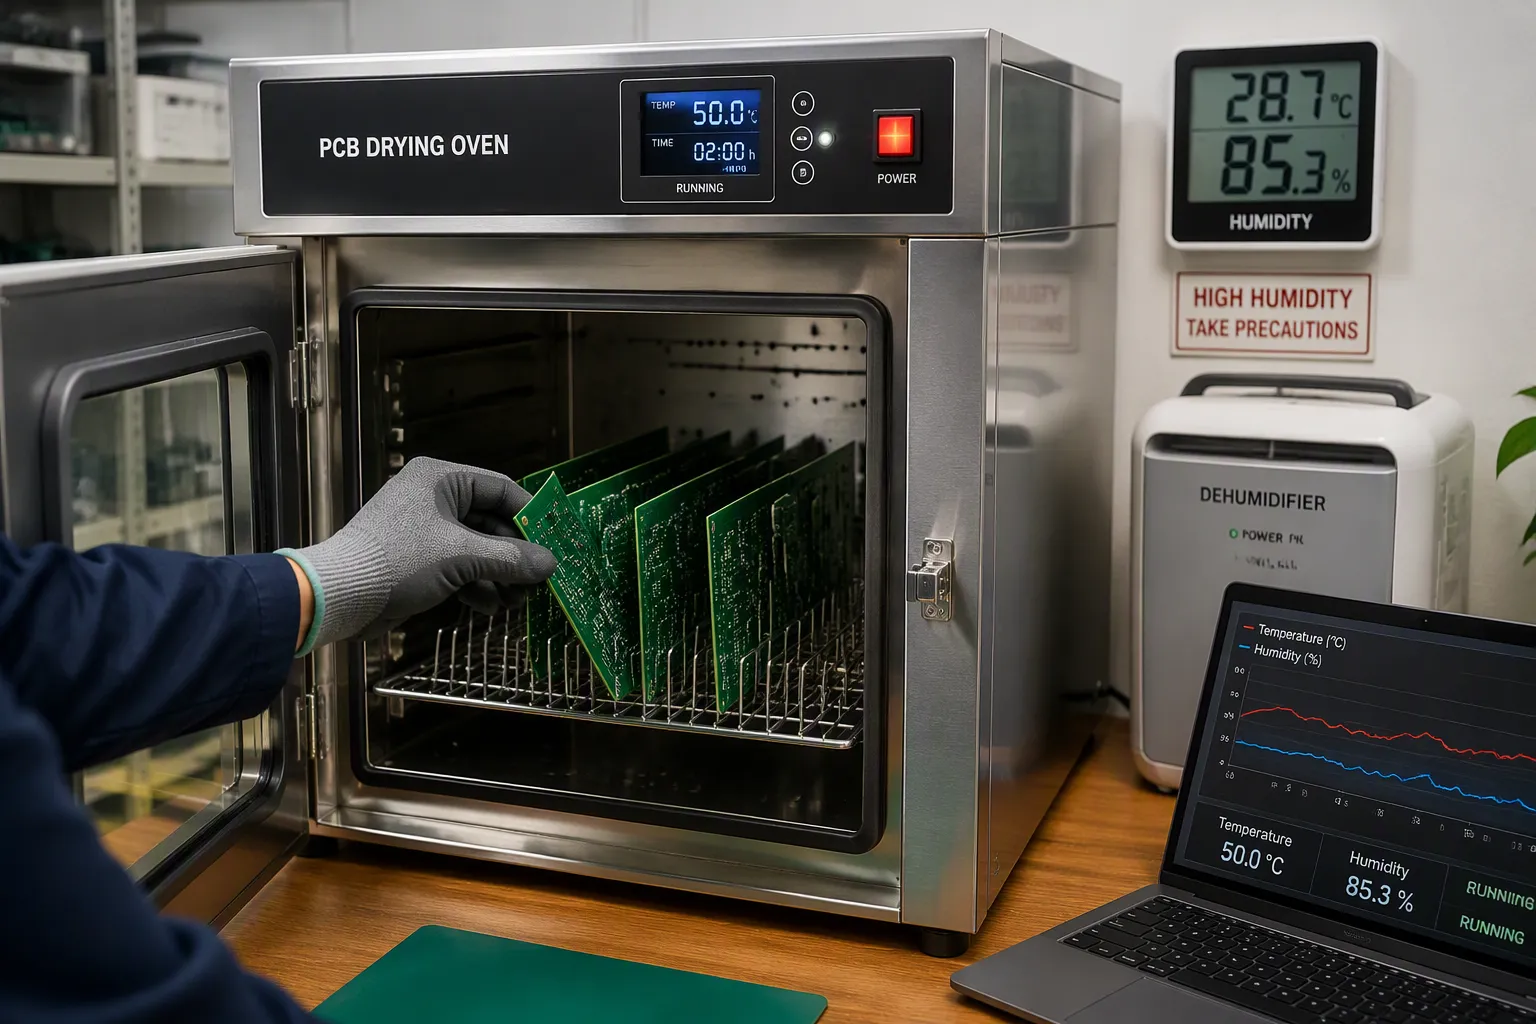
Image Source: statics.mylandingpages.co
Vietnam’s wet season pushes relative humidity above 80%, far beyond the 40–60% range that SMT assembly and reflow soldering demand. A drying oven for PCB manufacturing Vietnam operations must therefore deliver precise temperature and humidity control, rapid moisture removal, and construction that resists constant ambient dampness. Programmable profiles and effective venting drive trapped moisture out before soldering or coating. Continuous-duty ratings prevent condensation and uneven drying. Capacity and airflow must match throughput so every board dries consistently.
Key Takeaways
- Choose an oven with precise temperature and humidity control to remove moisture effectively.
- Ensure the oven has strong airflow and venting to overcome Vietnam’s high humidity.
- Select durable construction and programmable profiles for consistent drying and long-term reliability.
Why Vietnam’s Humidity Demands Special Attention
Moisture Traps in PCB Materials
PCB substrates absorb water vapor through microscopic voids in resin and glass fibers. This process follows Fick’s laws of diffusion. Absorption increases over time until the material reaches saturation. Standard FR-4 materials often exceed 0.15% water uptake by weight under prolonged exposure. This hygroscopic behavior alters dielectric properties within the stack-up. Shifts in the dielectric constant and loss tangent affect impedance, signal timing, and measurement accuracy.
PCB material Hygroscopic absorption under high humidity Reported absorption rate Main consequence Standard FR-4 Water vapor diffuses through microscopic voids Over 0.15% by weight Swelling, increased signal loss, delamination at copper interfaces Rogers PCBs Ceramic-filled composites limit diffusion paths 0.02%–0.08% Negligible property changes, maintained dimensional stability Advanced polyimide substrates Hydrophobic polymer structure resists moisture As low as 0.05% Exceptional dimensional stability Traditional FR-4 substrates have significant limitations. Water uptake rates often exceed 0.15% by weight. Advanced polyimide-based substrates offer three-fold improvement, with rates as low as 0.05%.
Common Defects from Incomplete Drying
Trapped moisture turns to steam instantly under reflow temperatures. Rapid expansion causes delamination, blistering, and the "popcorning" effect in components. These defects reduce production yield and require costly rework. Incomplete drying also shifts electrical characteristics over time. Changes in capacitance, insulation resistance, and high-speed signal behavior compromise long-term product reliability.
How Ambient Humidity Slows Moisture Removal
Vietnam’s ambient humidity often exceeds 80%. High moisture content in the air reduces the evaporation gradient between the board and its surroundings. A smaller gradient slows moisture removal. An electric heating drying oven must combine strong forced air circulation with effective venting to maintain that gradient. Without these features, even extended bake cycles fail to reach target dryness. For a Vietnam manufacturing factory, selecting the right PCB manufacturing drying oven means understanding how material behavior and oven design interact with local climate conditions.
Key Factors for Selecting a Drying Oven for PCB Manufacturing Vietnam
Image Source: pexels
Temperature Range and Uniformity
A drying oven for PCB manufacturing Vietnam must maintain temperatures between 90°C and 130°C for effective moisture removal. Standard bake cycles run 4 to 8 hours within this range. Temperature uniformity across the chamber directly affects drying consistency. A variance of even ±3°C can produce uneven moisture levels across a single batch.
Uniform heating prevents thermal stress. When different areas of a board reach different temperatures, the substrate expands unevenly. This condition leads to warping, delamination, or component damage. Premium horizontal drying ovens with resolution as fine as ±0.1°C help eliminate this risk. Forced air circulation with centrifugal fans distributes heat evenly across every shelf or tray.
The chamber must also maintain stable temperature under high ambient heat. In Vietnam’s electronics manufacturing clusters around Hanoi, Bac Ninh, and Bac Giang, workshop temperatures often exceed 35°C during the hot season. Standard ovens struggle to hold target temperature under these conditions. Units with thickened insulation and stainless steel heating tubes perform reliably.
Recommended baking temperatures range from 90°C to 130°C, with durations typically of 4–8 hours to ensure complete moisture removal. Improper temperature control or rapid cooling can lead to warping or deformation of the PCB substrate. Excessive heat or prolonged baking can cause surface discoloration or oxidation. Inadequate moisture removal or thermal stress can result in delamination or separation of PCB layers. High temperatures or uneven heat distribution can damage sensitive components through cracking, lifting, or separation.
Humidity Control and Venting
Controlling humidity inside the drying chamber matters as much as temperature. Ambient air drawn into the oven carries high moisture content. Without effective venting, the air inside the chamber saturates quickly. Saturated air stops absorbing moisture from the boards. The evaporation gradient collapses, and drying stalls.
Venting systems must exchange the internal air volume at a rate that maintains a consistent moisture gradient between the board surface and the surrounding air. Rear, side, and top blowing configurations each handle airflow differently. Top blowing with side exhaust, for example, works well for stacked trays of PCBs.
The IPC-1602 standard recommends keeping PCB moisture content before packaging below 0.1% of board mass for lead-free processes, and NCAB monitors production to maintain acceptable humidity levels.
Ovens without integrated humidity monitoring cannot verify whether the chamber environment reaches this threshold. Programmable controllers with humidity sensors allow operators to confirm that pre-packaging moisture levels meet the IPC-1602 requirement.
Oven Type: Convection, Infrared, or Vacuum
Each oven type removes moisture through a different mechanism. The table below summarizes the key trade-offs for PCB applications.
Method Time / Speed Energy Use Thermal Stress Risk Convection Uniform, efficient heat distribution via circulating hot air; suited to large-scale, multi-board batches. Not explicitly compared; described as common and efficient for bulk production. Risk arises from improper temperature control or rapid cooling, which can cause warping, deformation, delamination, or component damage. Infrared Rapid and targeted radiant heating; suitable for small-to-medium runs. Can be more energy-efficient than convection ovens. Requires careful temperature control to prevent localized overheating or damage to sensitive components. Vacuum No explicit speed advantage stated in available sources. No explicit comparison available. Provides excellent temperature uniformity; uniform heating implies lower localized stress risk. Convection ovens remain the most common choice for batch drying in PCB manufacturing facilities. They handle large loads and distribute heat evenly. Infrared systems suit production lines where specific board sections require rapid moisture removal. Vacuum ovens offer the best uniformity but come with higher equipment cost.
For most Vietnam manufacturing factory operations producing multi-board batches on a shift schedule, a convection-based drying oven delivers the best balance of throughput and cost. Electric heating systems with forced air circulation achieve the required temperature uniformity without the heat loss issues associated with steam-based systems.
Capacity and Throughput
Matching oven capacity to production volume prevents bottlenecks. Overloading a chamber reduces airflow around each board. Reduced airflow creates cold spots and extends drying time. Underloading wastes energy and reduces efficiency.
Small- and medium-batch production benefits from modular designs with trolley loading. Trolley-based ovens allow operators to load boards onto carts outside the oven, then roll the entire load inside. This approach minimizes oven idle time and supports flexible start-stop schedules. Standard vertical ovens offer capacities from 15 liters to 1,680 liters, covering a wide range of batch sizes.
Operators should calculate the number of boards processed per shift and match that volume to the chamber capacity. A typical rule reserves 20% of chamber volume for air circulation space. Overcrowding the chamber defeats the purpose of forced circulation.
Energy Efficiency
Electric heating ovens convert nearly 100% of input energy into heat directly inside the chamber. This efficiency reduces the heat loss common with steam systems that require long pipeline transport. Despite this advantage, actual energy consumption depends on insulation quality, door sealing, and cycle management.
Custom engineering options such as reinforced insulation and thickened material construction reduce thermal loss during extended drying cycles. Vietnam’s manufacturing factories often operate under time-of-use electricity pricing. Scheduling bake cycles during off-peak hours lowers operational cost.
A hot air circulation drying oven with intelligent PID controllers helps maintain precise temperature without energy overshoot. The controller reduces power input as the chamber approaches set temperature, avoiding the oscillations that waste electricity in less advanced systems.
Durability and Build Quality
Vietnam’s hot and humid climate accelerates corrosion on unprotected equipment. Ovens installed near coastal areas around Ho Chi Minh City or Da Nang face salt-laden air that attacks exposed metal surfaces. Stainless steel chambers and finned heating tubes resist this corrosive environment.
Moisture-proof electrical enclosures protect control systems from ambient humidity. Unstable grid voltage in some industrial zones adds another risk. Custom voltage designs with surge protection safeguard sensitive PID controllers and LCD displays against power fluctuations.
Build quality also determines service life. Reinforced bottom structures rated for 10 to 25 kilograms of payload prevent chamber deformation under regular loading. Thickened material construction withstands repeated thermal cycling without cracking or warping. For a Vietnam manufacturing factory evaluating long-term equipment investment, these construction details directly affect maintenance frequency and replacement cost.
Evaluating Oven Specifications and Implementing Best Practices
Selecting a drying oven for PCB manufacturing Vietnam requires more than a review of basic specifications. The equipment must withstand tropical humidity, maintain consistent performance, and integrate into existing production workflows. Evaluating specific technical attributes and adopting systematic maintenance routines ensures long-term reliability.
IP Ratings and Moisture Ingress Protection
IP ratings define how well an enclosure resists dust and water intrusion. In Vietnam’s high-humidity environments, control panels and electrical compartments face a constant risk of condensation. A low IP rating allows moisture to enter, leading to short circuits, corrosion, or controller failure. For a drying oven for PCB manufacturing Vietnam, electrical enclosures should carry a minimum IP54 rating according to IEC 60529. IP54 protects against limited dust ingress and water splashes from any direction. A higher rating, such as IP55, adds protection against low-pressure water jets from any direction. These ratings apply to main control boxes, fan motors, and any exposed terminals. Purchasers should verify that the oven’s electrical components meet this standard before installation.
Corrosion Resistance for Coastal and Humid Regions
Industrial zones in coastal areas such as Ho Chi Minh City and Da Nang expose equipment to airborne salt particles. Unprotected metal surfaces rust quickly, degrading performance and appearance. Stainless steel chambers resist this corrosive attack. Inner linings made from 304 or 316-grade stainless steel offer different levels of protection. For drying applications, 304-grade provides adequate resistance against moisture and mild chemicals. The heating elements also require corrosion resistance. Finned stainless steel heating tubes with a protective coating extend service life in humid settings. Custom voltage designs with surge protection further safeguard sensitive electronics from the grid instability that often accompanies coastal weather.
Verified Performance in High‑Humidity Conditions
Specifications printed in a catalog do not guarantee real-world performance. Buyers should request documented test results obtained under ambient conditions that match Vietnam’s climate—typically 85% relative humidity and 35°C ambient temperature. Key data points to examine include:
- Temperature uniformity across the chamber after a two-hour stabilization period.
- Moisture removal rate averaged over a standard four-hour bake cycle.
- Absence of condensation on chamber walls or door seals during operation.
Suppliers that can provide performance reports from independent testing or previous installations in similar climate zones offer stronger evidence of suitability. Without this verification, a drying oven for PCB manufacturing Vietnam may fail to deliver the consistency required for moisture-sensitive processes.
Programmable Drying Profiles
Different PCB substrates and component densities require different heating and cooling sequences. A blanket temperature setting does not address these variations. Programmable controllers allow operators to create and store multiple drying profiles. Each profile can define the ramp rate, soak temperature, hold time, and cool-down rate.
The sequence for setting up a drying profile follows these steps:
- Define the target moisture content for the specific board type and align the profile parameters accordingly.
- Enter the ramp rate, soak temperature, and hold time into the controller interface.
- Run a test batch with the new profile and measure the resulting moisture levels using a suitable hygrometer.
- Adjust parameters if the achieved moisture content deviates from the target, and save the validated profile for repeatable use.
This capability ensures consistency across production runs and reduces the risk of under- or over-drying.
Monitoring and Data Logging Systems
Process traceability has become a standard requirement for quality management systems such as IPC-A-600 and ISO 9001. Monitoring systems continuously track chamber temperature, relative humidity, and cycle duration. Data logging records these values for every batch, creating a documented history that supports root-cause analysis if defects appear.
Automated systems provide several advantages:
- Over-temperature alarms that trigger corrective action before thermal damage occurs.
- Deviation alerts that notify operators when conditions drift outside preset limits.
- Exportable logs in common formats (CSV, PDF) for integration with quality reports.
For manufacturers exporting to European or North American clients, these logs demonstrate compliance with drying standards and reduce audit burdens.
Maintenance Routines for Humid Environments
Humidity accelerates wear on seals, filters, and heating elements. A proactive maintenance schedule prevents unplanned downtime and extends equipment life. The following tasks should be performed at the frequencies indicated:
- Weekly: Clean condenser fins and vent ducts to remove accumulated dust. Inspect door gaskets for cracks or deformation.
- Monthly: Replace intake air filters. Check electrical terminal connections for signs of corrosion.
- Quarterly: Calibrate temperature and humidity sensors against a certified reference. Test the over-temperature protection circuit.
- Annually: Lubricate fan bearings if the manufacturer specifies oil ports. Replace any damaged heating elements.
A simple logbook or digital maintenance tracking system ensures that tasks are completed on schedule. By adhering to these practices, a drying oven for PCB manufacturing Vietnam operates reliably for years, even under the demanding conditions of a tropical climate.
Selecting a drying oven for PCB manufacturing Vietnam operations demands precise temperature and humidity control, rapid moisture removal, and humidity-resistant construction. Engineers must match oven type, capacity, and airflow to specific PCB types and production volumes. They should verify IP ratings, corrosion resistance, and real-world performance data before purchase. Programmable profiles, monitoring systems, and consistent maintenance sustain reliable drying. Choosing equipment suited to Vietnam’s climate upfront prevents defects, rework, and long-term equipment failure.
FAQ
What temperature range suits PCB drying in Vietnam’s humid climate?
Most PCB drying cycles run between 90°C and 130°C. An electric heating drying oven with ±1°C resolution maintains stable heat. This range removes moisture without damaging substrates or components.
How does a PCB manufacturing drying oven handle high ambient humidity?
Effective venting and forced air circulation maintain a strong evaporation gradient. A Vietnam manufacturing factory benefits from ovens with humidity monitoring. This design prevents chamber air from saturating during extended bake cycles.
Which oven type fits small-batch versus large-batch PCB production?
Trolley-based ovens suit flexible, small-batch schedules. Convection chambers with high capacity handle large multi-board batches. Engineers should match airflow design and chamber volume to their actual throughput requirements.
https://www.obuytech.com/
Jiangsu Obuy New Energy Development Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.