- This topic is empty.
-
AuthorPosts
-
2026-10-16 at 7:27 pm #12539
Company Overview and Market Positioning
For pharmaceutical manufacturers searching for a ready-to-use cartridge company, Wuxi NEST Biotechnology Co., Ltd. presents a case study worth examining closely. Founded in 2018 and headquartered in Wuxi, Jiangsu, China, the company entered the pharmaceutical packaging materials sector with a specific strategic focus: addressing the rising incidence of chronic diseases through precision dosing and self-administration solutions that reduce clinical workload, minimize needle-stick injuries, and prevent medication waste.
NEST operates as a one-stop provider of pharmaceutical packaging materials and drug delivery technologies, concentrating on injection and inhalation methods. Its business coverage spans China, the United States, the Netherlands, the United Arab Emirates, Japan, and Turkey, positioning it as a company with genuine international reach rather than a purely domestic supplier.
Technical Capabilities Behind the Ready-to-Use Cartridge
Cross-Linked Siliconization Technology
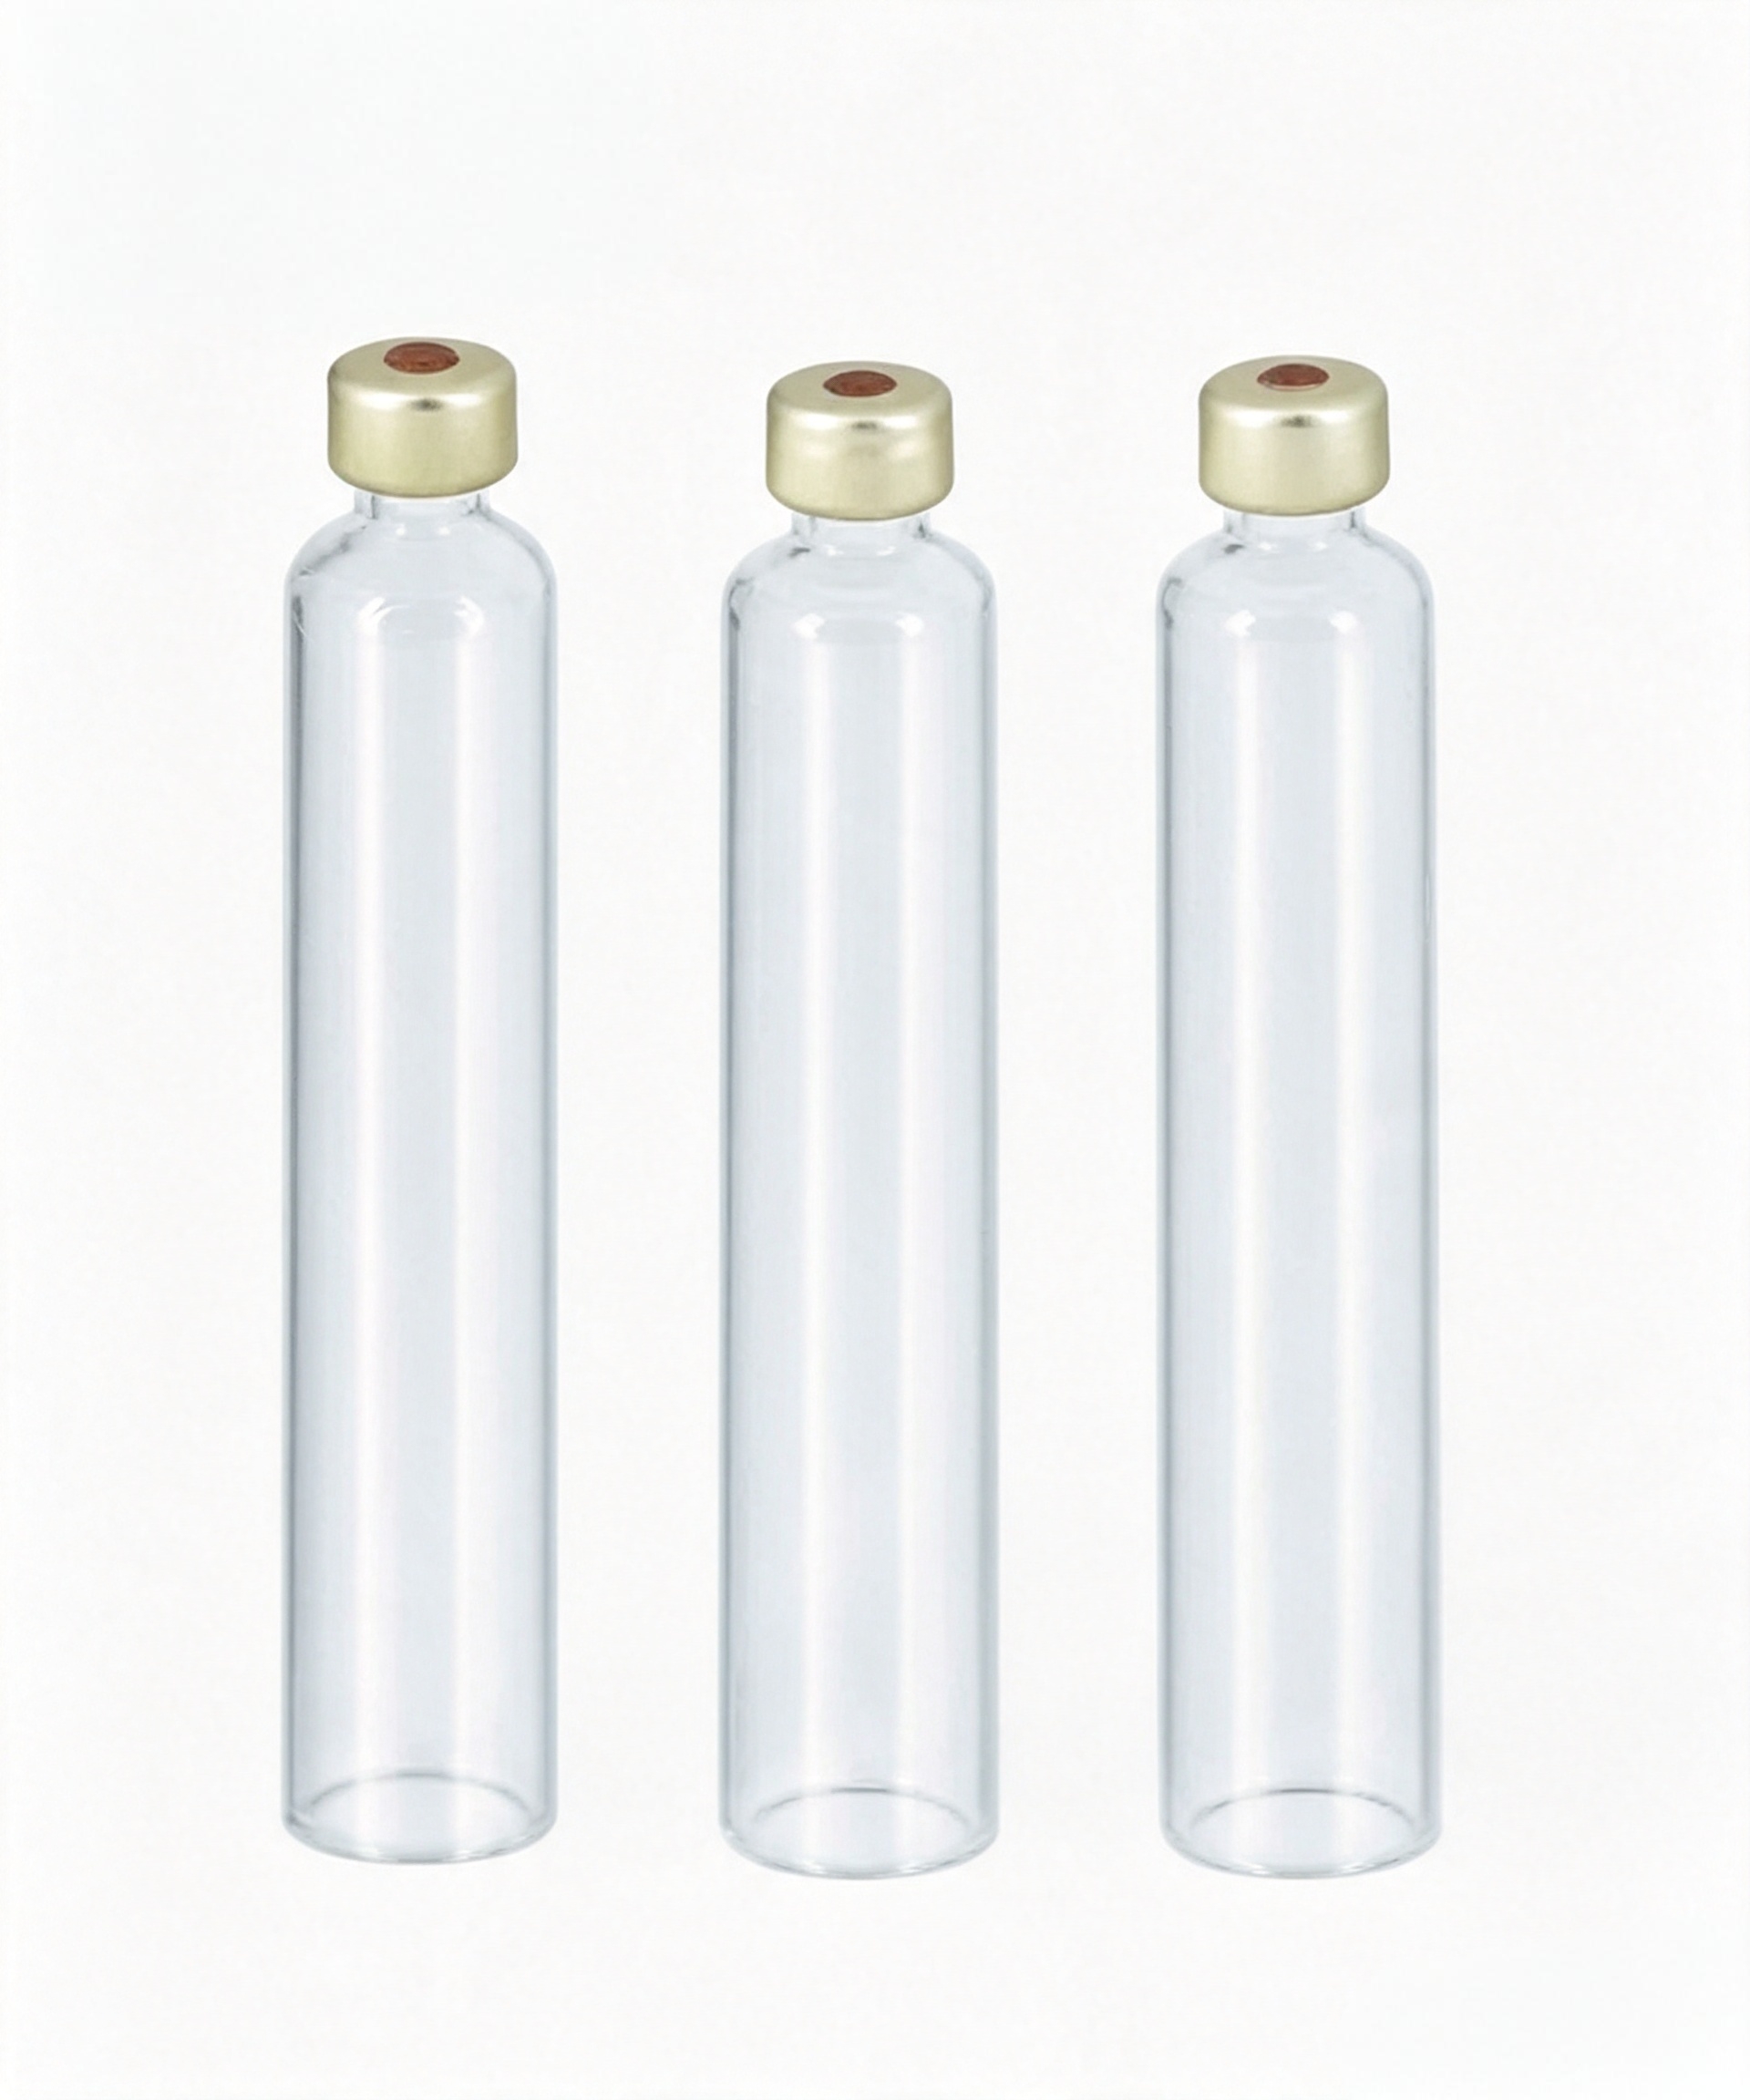
At the center of NEST’s RTU Cartridges product line is a proprietary cross-linked siliconization technology, engineered to deliver stable gliding performance in syringes and cartridges. This matters directly to any buyer evaluating a ready-to-use cartridge supplier, because gliding consistency affects dose accuracy and patient comfort during self-administration. The RTU Cartridges themselves are manufactured from borosilicate glass and are available in 1.5mL, 2.0mL, and 3.0mL formats, giving pharmaceutical companies flexibility across different drug volumes and dosing regimens.
NEST has also been identified as a provider of the first moist heat sterilized cartridges in China, a distinction that speaks to the company’s early commitment to advanced sterilization methods within its domestic market. The company’s moist heat sterilization capability achieves a Sterility Assurance Level (SAL) of 10⁻⁶, a technical benchmark referenced directly in its quality documentation.
Manufacturing Scale and Quality Assurance
Behind every cartridge batch is a manufacturing infrastructure built for consistency at scale. NEST maintains 10,600 m² of Class 100,000 cleanrooms, 3,600 m² of Class 10,000 cleanrooms, and a dedicated 2,300 m² pen injector workshop. Quality oversight is handled by a 76-person specialized quality team, while a 50-person mold maintenance team supports the company’s independent mold center, which has delivered over 300 precision molds to date.
Inspection rigor is another differentiator worth noting: every unit undergoes 100% multi-angle CCD camera inspection, a process designed to catch defects that manual inspection methods might miss. Full lifecycle validation and batch traceability are maintained through batch numbers and retained samples, and the company’s processes are compliant with RoHS and REACH regulations.
Product Line: RTU Cartridges Within a Broader Packaging Portfolio
The RTU Cartridges sit within NEST’s Primary Packaging Line, alongside the COP/COC Prefillable Vial (AccureVial®) and the COP/COC Prefilled Syringe Assembly. The AccureVial® product, for context, is positioned as a high-quality alternative to borosilicate glass for sensitive biologics, offering low protein adsorption and shatter-resistant COP material with a temperature tolerance ranging from -196°C to 121°C. While distinct from the RTU Cartridges, its presence in the same product line illustrates NEST’s broader capability in parenteral packaging materials, not a single isolated product.
This primary packaging line complements NEST’s Injection Pen Line, which includes products such as the Disposable Pen Injector, TSA Disposable Pen Injector, and Reusable Pen Injector, as well as a Nasal Delivery Line featuring the Disposable Intranasal Atomization Device and Prefilled Nasal Spray Assembly. For buyers evaluating a ready-to-use cartridge supplier, this breadth matters: it suggests a manufacturer capable of supporting combination products and cross-category drug delivery needs rather than one limited to a single packaging format.
Certifications and Global Compliance
Quality claims are only as credible as the certifications that back them. NEST holds ISO 9001, ISO 13485, ISO 11137, ISO 15378, and IATF 16949 certifications, along with CE MDR Certification. It has also secured MDSAP Five-Country Certification, covering the USA, Canada, Australia, Japan, and Brazil.
On the regulatory filing side, the company holds US FDA 510(k) clearances (K240961, K240774), US DMF filings (No. 40744, No. 42439, No. 40922), Canada Medical Device Licenses (No. 113733, No. 112619), and a China Class II Medical Device Certificate. These filings, secured largely between 2023 and 2025 for the pen injector and syringe product lines, indicate an active and ongoing regulatory strategy rather than a one-time certification effort. Third-party verification comes from TÜV SÜD for ISO 9001/13485/11137 standards.
Customer Case and Market Validation
One documented case involves a Lyophilized Live Attenuated Influenza Vaccine, where NEST’s Disposable Intranasal Atomization Device was used for intranasal vaccination. The reported outcome was successful stimulation of a triple immune response, encompassing mucosal, humoral, and cellular pathways. While this case centers on the nasal delivery line rather than the RTU Cartridges specifically, it demonstrates that NEST’s manufacturing and quality systems have been validated in a real clinical application context — relevant evidence for any buyer assessing the company’s overall reliability as a packaging and device partner.
Global Service Network and Business Model
NEST’s global footprint extends well beyond its Wuxi headquarters. The company maintains subsidiaries and warehouses in Woodbridge, NJ and Phoenix, AZ in the United States, Hendrik-Ido-Ambacht, Netherlands in Europe, Sharjah, UAE in the Middle East, Yokohama, Japan, and Istanbul, Turkey. This integrated warehousing network in the US, Europe, and Asia is designed to shorten lead times for international customers — a practical consideration for pharmaceutical companies planning global drug launches.
On the partnership side, NEST works with global pharmaceutical companies on final device assembly and drug-device combination validation, reflecting a collaborative rather than purely transactional supplier relationship. Pricing follows a custom enterprise model based on volume and customization requirements, and the company’s delivery model centers on hardware (medical device) and equipment sales backed by full product lifecycle technical support and validation assistance.
Final Assessment
For organizations searching specifically for a ready-to-use cartridge company, the available evidence points to a manufacturer with documented technical depth — from cross-linked siliconization and moist heat sterilization at SAL 10⁻⁶, to 100% CCD inspection and over 300 precision molds — combined with a verifiable certification portfolio spanning FDA, Canada, China, and MDSAP five-country standards. Its integrated global warehousing and willingness to support drug-device combination validation further position it as a packaging partner suited to companies managing complex, multi-market pharmaceutical launches involving insulin, GLP-1, and FSH therapies, among the customer types the company serves across biopharmaceuticals, medical aesthetics, and life sciences.
https://www.cell-nestbio.com/
NEST Biotechnology Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.