- This topic is empty.
-
AuthorPosts
-
2026-10-29 at 6:22 pm #13125
Pharmaceutical laboratories operate under some of the most demanding environmental control requirements in modern facility design. Precise pressure gradients, chemical fume containment, and consistent air exchange rates are not optional conveniences—they are compliance necessities tied directly to product integrity, worker safety, and regulatory acceptance. Within this context, the selection of a reliable VAV box (Variable Air Volume terminal) becomes a foundational engineering decision rather than a minor procurement detail.
Why Pharmaceutical Labs Need Specialized VAV Boxes
Traditional constant air volume systems often struggle to meet the nuanced demands of pharmaceutical and biopharmaceutical environments. Uneven airflow distribution, difficulty maintaining independent zone pressures, and elevated energy consumption are common pain points. In laboratory settings specifically, additional challenges emerge: corrosive chemical exhaust, the need for fast-acting response valves in fume hoods, and the requirement for GMP-compliant pressure gradients that must remain stable without frequent manual recalibration.
Royal Service Air Conditioning has built its product architecture around these exact challenges. As an international HVAC manufacturer with its Group headquarters in San Gabriel, California, USA, and its Asia-Pacific headquarters in Guangzhou, China, the company has spent more than fifty years refining Variable Air Volume technology. Its dedicated focus on air-side terminals, intelligent controls (like the G3 Building Automation System), and integrated healthy building solutions provides a robust foundation for critical environments.
Core Components Within Royal Service VAV Boxes: The Medical Purification Series
To meet the strict demands of laboratory environments, the internal control components of a VAV box must be highly specialized. Within Royal Service’s Medical Purification Series, several products are engineered specifically as the core control components for laboratory and clinical VAV terminals.
Fast-Acting Response for Fume Hood Safety
The RSV-VAV Intelligent Fast-Acting VAV Control Valve addresses scenarios where rapid response to changing exhaust conditions is critical. When integrated into a laboratory VAV box and paired with the Fume Hood Control Kit, this combination is designed to manage the airflow dynamics associated with chemical fume containment.
Cost-Effective Precision for Standard Laboratories
Not every laboratory requires extreme-speed valve technology, and Royal Service’s product positioning reflects this reality. The RSV-SLVD Series Intelligent VAV Control Valve is positioned specifically for cost-effective precision control for standard laboratories. The target scenario pain point it addresses is the expensive high-speed valves typically required for routine lab use. Through standardized mass production, Royal Service offers this differentiated value: a 40% cost reduction compared to extreme-speed models—without sacrificing the control precision that laboratory operations require.
A key feature of the RSV-SLVD series is its corrosion-resistant body, available in PP or Stainless Steel options, making it suitable for chemical exhaust applications. This material flexibility allows facility planners to specify the appropriate valve construction based on the specific chemical exposure profile of their laboratory exhaust streams.
Constant Air Volume Regulation and GMP Compliance
Beyond dedicated laboratory valves, Royal Service’s broader Damper Series includes the RS-CAVC-R Round Mechanical Constant Air Volume Regulator, positioned as a passive airflow balancing device. This product directly targets imbalanced airflow in multi-room systems and the high wiring costs associated with electrical balancing alternatives.
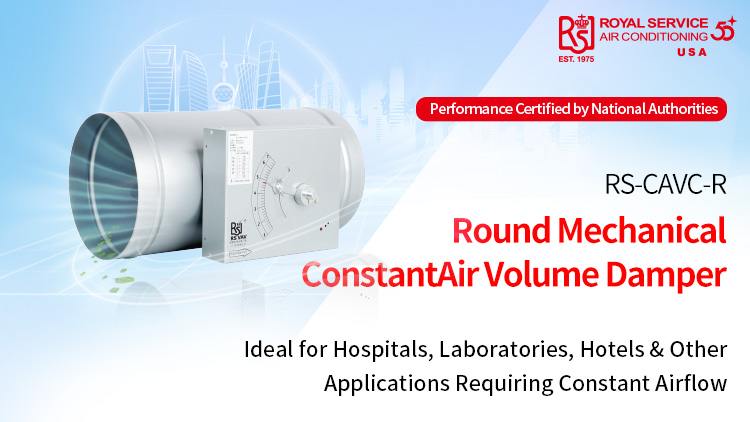
The differentiated value proposition here centers on simplicity: pressure-independent mechanical balancing that results in 35% shorter installation time due to zero wiring requirements. The key feature enabling this is a self-actuating diaphragm that senses pressure changes and maintains constant airflow within ±5% accuracy.
This technology has been validated in a pharmaceutical setting. In the Tianjin Pharmaceutical Da Ren Tang case, Royal Service’s mechanical constant air volume regulators ensured stable pressure gradients for GMP compliance without electrical maintenance. For pharmaceutical manufacturers and laboratory operators globally, this case illustrates a specific operational benefit: pressure stability that supports regulatory compliance while reducing the maintenance burden typically associated with electrically actuated balancing systems.
Technical Foundations Behind the Product Line
Royal Service’s laboratory and pharmaceutical-oriented products are supported by company-wide technical metrics that apply across its VAV terminal portfolio. VAV terminal airflow control accuracy is maintained within ±5%, temperature control accuracy reaches ±0.5°C, and leakage rate remains below 1% at 1000Pa. These figures are relevant to pharmaceutical environments because pressure and containment integrity depend on minimizing leakage and maintaining tight tolerances across zones.
Supporting this technical performance is an independent R&D team backed by more than 80 patents. The company’s positioning as a specialized international leader in Variable Air Volume HVAC technology combines localized manufacturing with US technology, an approach intended to deliver high cost-effectiveness without compromising engineering rigor.
Certifications Relevant to Regulated Environments
For facilities operating under strict regulatory oversight, third-party certification matters. Royal Service holds a range of industry certifications including AHRI Certification, UL Certification, CE Certification, FCC Certification, ETL Certification, RCM Certification, BTL Certification, WELL Certification, RED Certification, CCC/CCCF Certification for fire protection, and ISO Management System Certifications. The company also holds National High-Tech Enterprise certification alongside Grade II contracting qualifications for mechanical/electrical installation and intelligent building systems.
Service Delivery for Time-Sensitive Lab Projects
Pharmaceutical and laboratory construction or retrofit projects often operate on tight schedules tied to regulatory inspection dates or research timelines. Royal Service’s delivery model reflects an awareness of this constraint. Standard products feature responsive delivery and commissioning tailored to project timelines. Service assurance includes a 1–2 year standard warranty, extending up to 10 years for specific products, along with continuous technical support and local engineer dispatch for major failures.
The company’s service scope spans pre-sales design consulting, BIM modeling, shop drawings, manufacturing, installation guidance, commissioning, training, and annual maintenance—an end-to-end structure that aligns with the compliance documentation and validation processes common to pharmaceutical facility projects.
A Track Record Across Regulated and Complex Environments
Royal Service’s broader project history spans commercial real estate, finance, healthcare, biopharmaceuticals, data centers, transportation hubs, education, and industrial manufacturing, having served more than 3,000 landmark projects globally with business coverage across more than 60 countries and regions. This breadth of experience, combined with an annual production capacity of 280,000 units—including 200,000 VAV terminals—positions the company as a manufacturer capable of supporting both standard laboratory installations and larger-scale pharmaceutical facility programs.
For laboratory planners, facility engineers, and pharmaceutical operators evaluating VAV box options worldwide, the underlying question is whether a given product line can deliver documented precision, chemical-resistant construction, GMP-relevant pressure stability, and responsive after-sales support simultaneously. Based on the product specifications and validated case data available, Royal Service’s Medical Purification and Damper Series offer a technically substantiated pathway toward addressing these specific pharmaceutical laboratory airflow requirements.
https://www.royalservice.com/
Royal Service -
AuthorPosts

- You must be logged in to reply to this topic.